
Home / Services / Rotor balancing / Vibration Diagnostics and Process Accuracy Checks of Industrial Equipment
Rotor balancing
Vibration Diagnostics and Process Accuracy Checks of Industrial Equipment
How a vibration survey shows the actual condition of rotary equipment, and how equipment and tooling are checked for process accuracy. We do not repair equipment: our part is the vibration survey and rotor balancing.
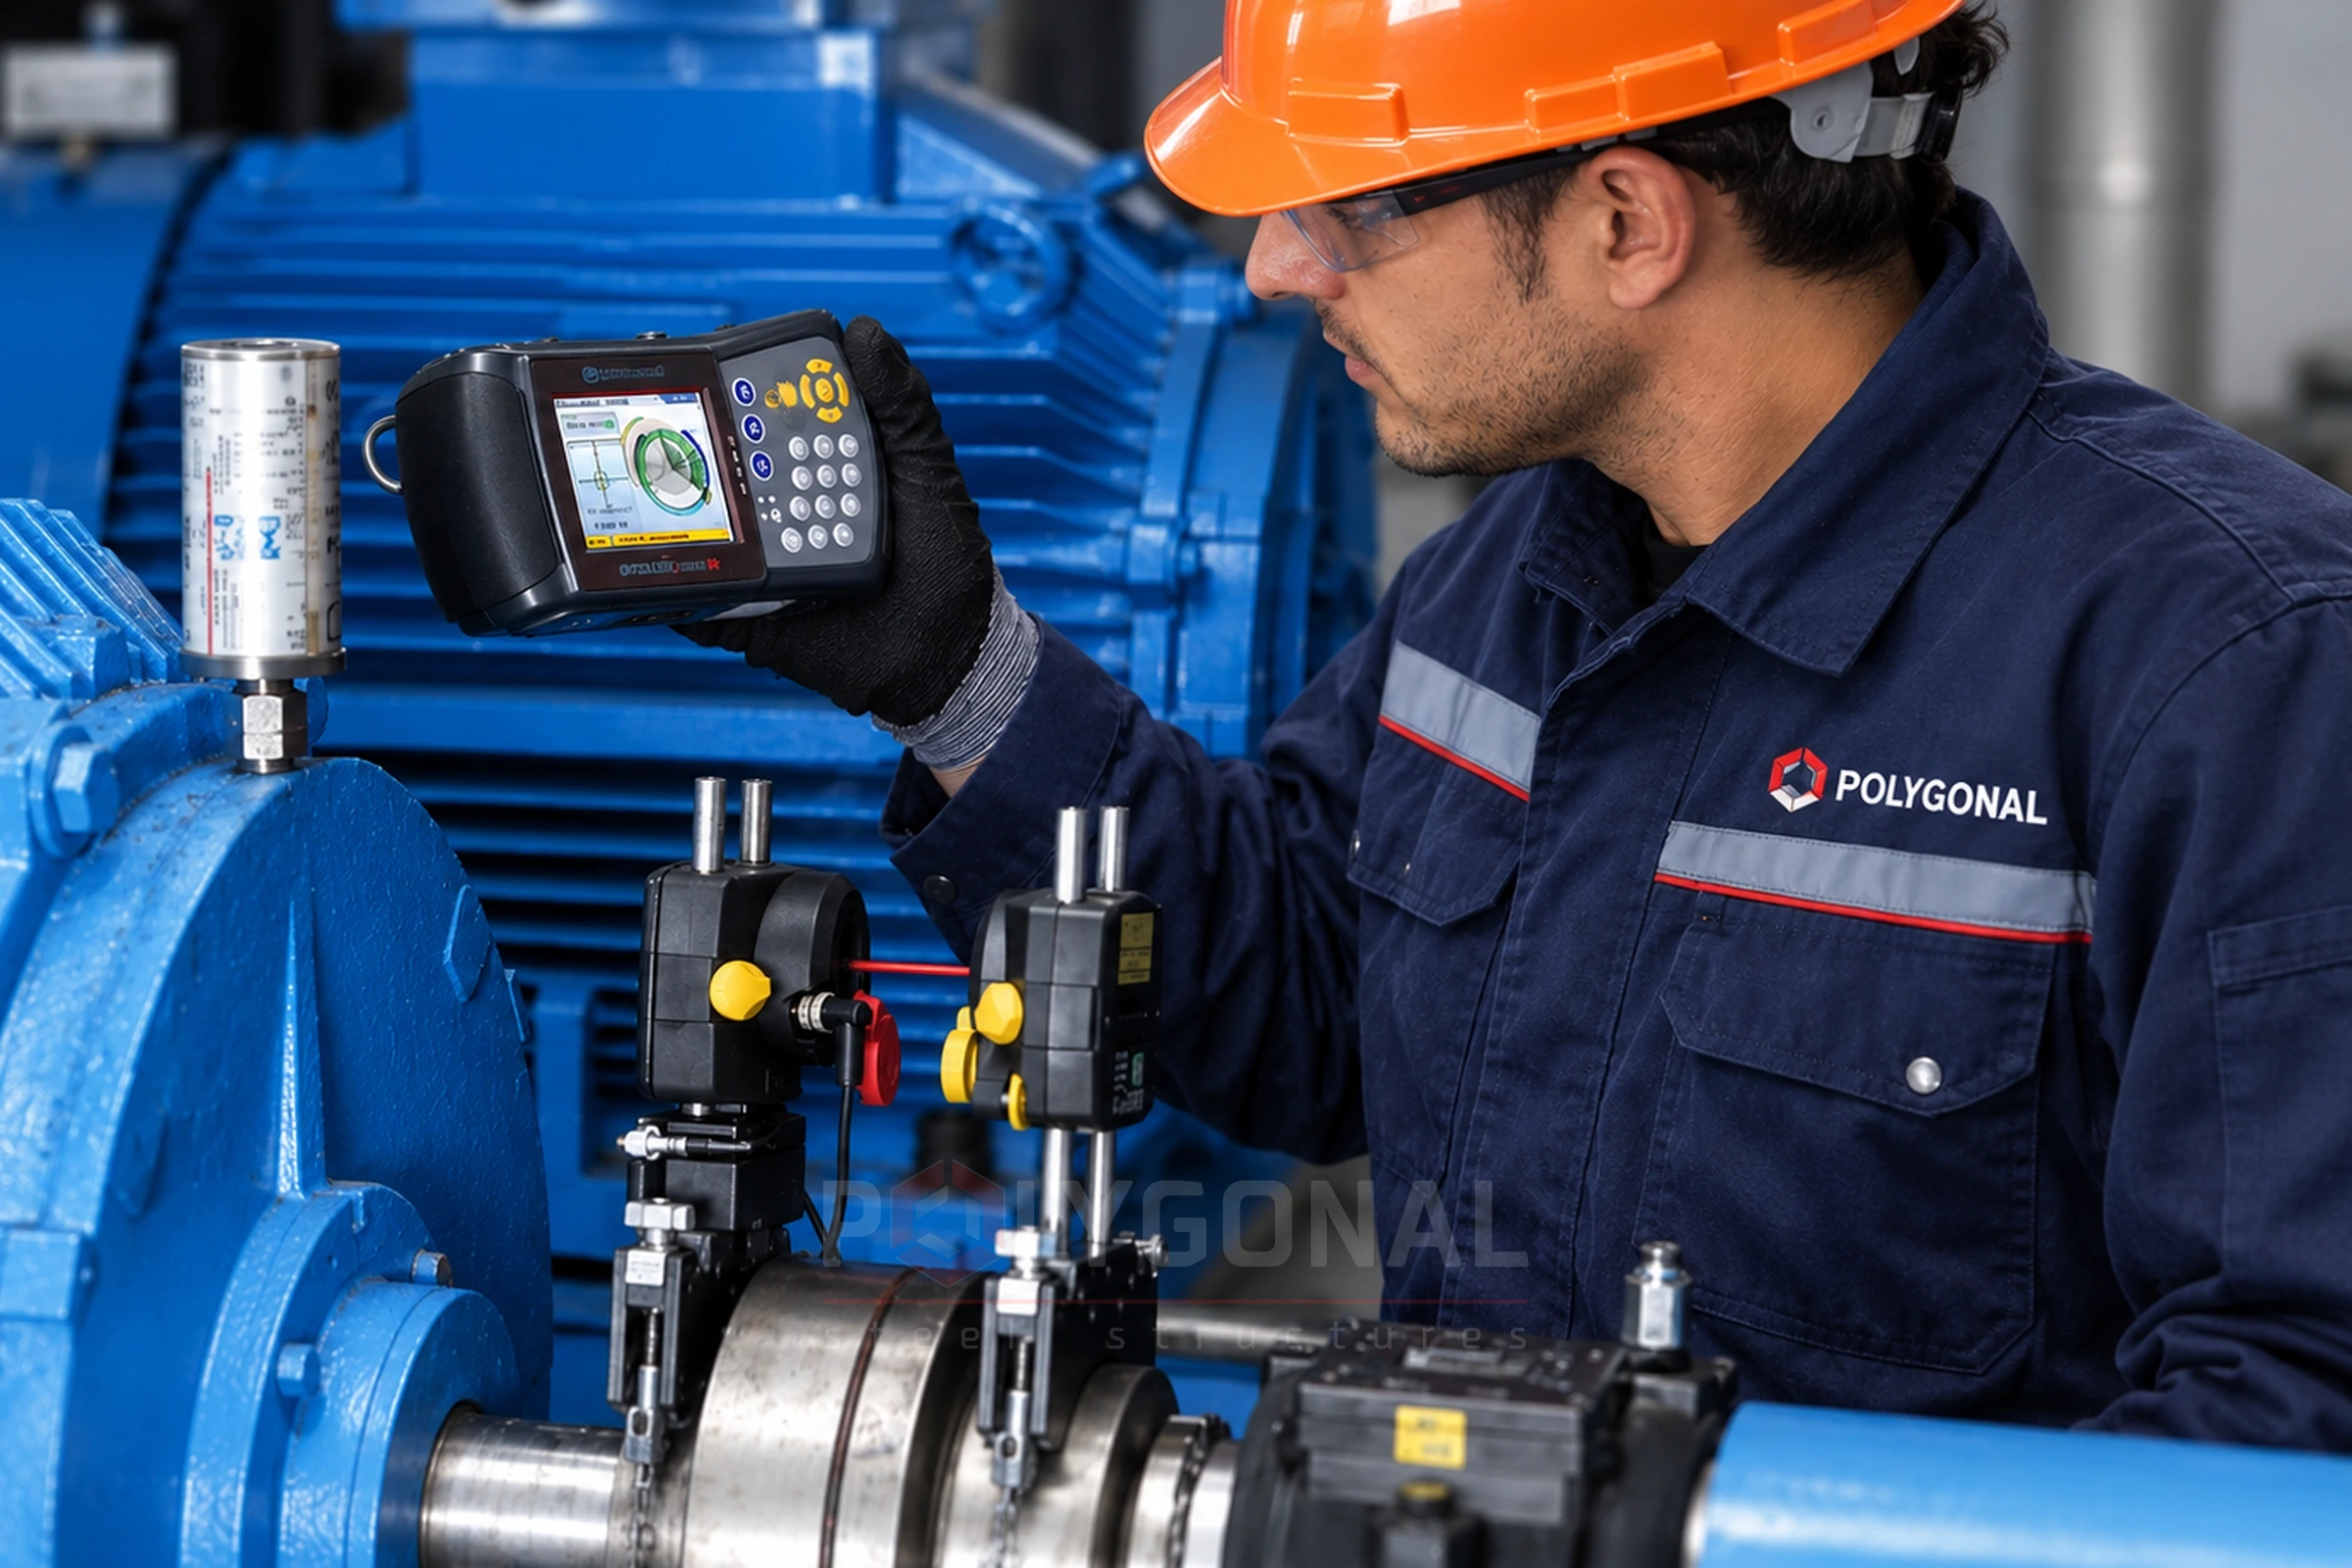
Vibration diagnostics of equipment
POLYGONAL surveys rotary equipment for vibration to establish its actual technical condition. Process equipment in industrial plants needs maintenance and repair all the time, and the best time to do it is when you know what state the machine is in right now. Repairs can then be cut to the minimum needed for trouble-free operation, and maintenance to a schedule (planned preventive maintenance) gives way to maintenance by actual condition.
A machine in working order runs at a low vibration level. That level is kept up by timely lubrication, tightening threaded connections, replacing parts that wear quickly, and adjustment: the position of shafts in space, the clearances in bearings, shaft alignment and rotor balancing. For rotary machines (electric motors, pumps, fans, turbines, generators), monitoring by vibration parameters is widespread worldwide. Vibration comes from forces acting inside the machine itself, so its signal carries information on the condition of the machine, its kinematic links and its individual units. Analysis of vibration signals gives reliable information on practically any defect of installation, manufacture or wear.
The most frequent questions on balancing and alignment concern industrial fans, induced draft fans and blowers. The impeller is symmetrical and turns fast (1000 rpm and more), yet the blades wear unevenly and the rotor goes out of balance. What a vibration survey gives you:
- see the real, current technical condition of machines;
- set the timing and scope of repair and adjustment work on a sound technical basis, and check how the work was done;
- cut the money and labour spent on operating equipment;
- lengthen the interval between repairs and the service life of machines, and reduce the need for spare parts, materials and equipment;
- meet “sudden” breakdowns and production stoppages less often.
Checking equipment and tooling for process accuracy
The accuracy of the fixtures and equipment used to make a product affects the quality of the output, so they are checked systematically. Tooling (dies, fixtures, assembly jigs) is checked mainly through the part made with it: whether the part conforms to the design and process documentation and, if it does not, what caused the deviation and what to correct. Equipment is checked differently: the measured accuracy parameters are compared with those given in the equipment data sheet.
Tooling is checked according to a schedule of tooling subject to checking and a schedule of periodic checks; the interval is set for each item separately. Fixtures not used since the last check are not checked, and the schedule is marked “not used”. The checking covers planned preventive maintenance of tooling on schedule, technical inspection, and checking of newly made and repaired fixtures.
In a periodic check, for example, the evenness of the gap between punch and die (coaxiality) is checked with a special punch and die: they are fitted and the punch is lowered into the die by hand. Blanking dies are tested by cutting cardboard or parchment. A clean cut along the whole contour means the gap is right; tearing or drawing of the parchment points to an uneven or excessive gap or blunt cutting edges. In bending and drawing dies, the checks cover the correct combination of profile elements and reliefs, the relative position of the upper and lower parts of the die, and whether the part’s profile matches the working drawing. In universal rulers, stops and locators, the linear dimensions they give are checked. The results go into the schedule with an assessment of condition: satisfactory, repair needed, not to be repaired or used.
All tooling in use gets a technical inspection twice a month. A commission examines it externally and measures the controlled dimensions of the part made on the fixture; the results go into a log. Tooling whose accuracy proves below the permitted level is repaired and checked again. If tooling is used without a check or with deviations from the documentation, the quality control department has the right to stop acceptance of products. Equipment is checked for process accuracy according to the schedule of equipment subject to checking and the annual schedule of planned preventive maintenance.
What we do ourselves
For rotary equipment our part of the work is a vibration survey and balancing of rotors in their own bearings. The method and the consequences of late balancing are covered in the articles Dynamic Rotor Balancing: Method and Stages and Consequences of Late Fan Impeller Balancing.
For the PPM system, the types of repair and maintenance, and the choice between scheduled and condition-based maintenance, see the article Industrial Equipment Maintenance and Repair.
Updated:
Vibration diagnostics and checking of equipment: frequently asked questions
What do we get from vibration diagnostics?
You see the actual technical condition of the machines, so you can set the timing and scope of repairs on a reasoned basis. It helps to lengthen the interval between repairs and to meet sudden breakdowns less often.
How often does tooling need to be checked for process accuracy?
All tooling in use gets a technical inspection twice a month. The interval for a full check is set separately for each item in the periodic-check schedule.
Is vibration diagnostics with balancing preventive maintenance or repair?
Vibration diagnostics does not repair anything by itself: it is monitoring, and the results decide whether action is needed. If vibration is merely rising and the unit keeps running, the balancing or alignment that follows stays within preventive, condition-based maintenance. Once a fault is found that cannot be put off, the same work becomes immediate corrective maintenance.
Do you repair equipment after the survey?
No. We do not repair equipment: our part is the vibration survey of rotary equipment and balancing of rotors in their own bearings. The survey shows the actual condition of the unit, so you can set the timing and scope of repairs on a reasoned basis.
Related products: Rotor balancing · Technical inspection
More on this topic: Dynamic Rotor Balancing: Method and Stages · Consequences of Late Fan Impeller Balancing · Industrial Equipment Maintenance and Repair
Get a quote for your requirements
Send us your requirements — we will calculate the price and lead time.